

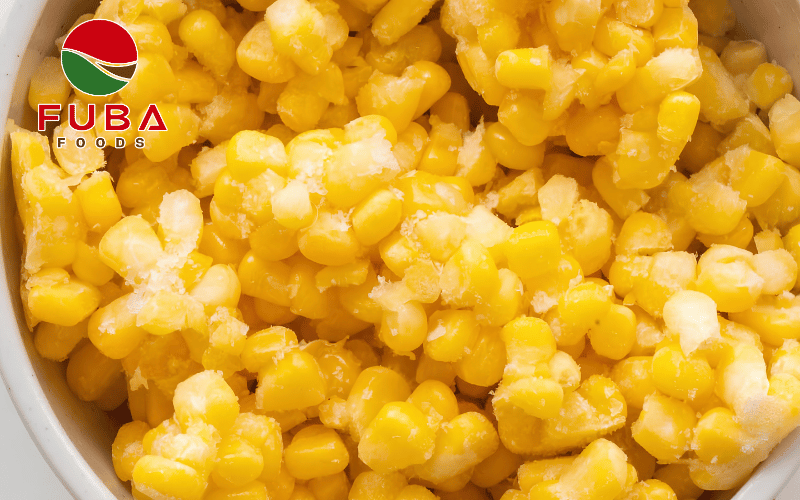
For importers, distributors, food manufacturers, foodservice operators, and retail businesses, choosing a frozen sweet corn supplier involves more than comparing prices. Consistent kernel quality, reliable supply, food-safety controls, suitable packaging, and dependable cold-chain management all influence whether the product can perform consistently after import.
A reliable frozen sweet corn supplier Vietnam should be able to connect agricultural sourcing with controlled processing, IQF freezing, quality inspection, cold storage, packaging, and export logistics. This integrated approach helps buyers reduce quality variation and manage frozen vegetable supply more predictably across international shipments.

This article looks at why Vietnam is becoming a practical sourcing base for frozen sweet corn, what determines product quality, how different frozen corn formats serve applications, and what buyers should evaluate when selecting a long-term supplier.
Why Source Frozen Sweet Corn from Vietnam?
Vietnam has become an increasingly relevant sourcing base for processed agricultural products, supported by diverse growing regions and a developing food-processing industry.
For buyers, however, agricultural availability alone does not guarantee a reliable frozen ingredient supply. The supplier must be able to convert suitable raw materials into consistent products while controlling processing, freezing, storage, packaging, and export requirements.
This is where Vietnam can offer a practical sourcing model. Sweet corn can be processed closer to the production area and converted into frozen formats suitable for international distribution, reducing some of the handling challenges associated with shipping fresh agricultural products over long distances.
A capable frozen sweet corn supplier Vietnam should therefore provide more than access to local corn. Buyers should evaluate the entire production system behind the finished product.
What Determines the Quality of Frozen Sweet Corn?
For industrial buyers, frozen sweet corn quality is influenced by several stages before and after freezing. Kernel maturity, size, color, sweetness, moisture, processing conditions, and freezing performance can all affect how the product performs in different applications.
Raw Material Selection and Consistency
The quality of frozen sweet corn starts with the raw material. Corn harvested at different maturity levels can vary in sweetness, texture, color, and moisture content.
These differences may affect cooking performance, formulation, portion control, and the appearance of finished products. For manufacturers working with standardized recipes, consistent raw material is therefore an important part of maintaining consistent finished-product quality.

A reliable supplier should have defined criteria for incoming raw materials and a sourcing system capable of supporting repeat production rather than relying on inconsistent spot purchases.
Processing and Preparation
After harvesting, sweet corn needs to undergo appropriate cleaning, sorting, preparation, and processing before freezing.
The specific preparation method depends on the final product format. Kernels may require cutting and separation, while cob-cut products require controlled sizing. Consistent preparation helps ensure that the frozen product matches the specification agreed upon with the buyer.
For large-volume procurement, controlled processing can also reduce variation between production batches and make it easier for manufacturers to maintain their existing recipes and production parameters.
Why IQF Technology Matters for Frozen Sweet Corn
IQF, or Individual Quick Freezing, rapidly freezes individual pieces of food rather than allowing them to form one solid frozen mass.
For sweet corn kernels, this format provides an important practical advantage: buyers can portion the quantity required for production without thawing an entire block. Individual frozen kernels are also easier to handle, measure, and incorporate into automated or semi-automated production processes.
IQF freezing can also help maintain the product’s characteristic color, texture, and flavor when the process is properly controlled. For buyers, the value of the technology therefore lies not only in freezing the product but also in creating a practical and consistent ingredient format.
FUBA uses multiple IQF freezing lines as part of its frozen food processing operations, alongside other freezing systems and inspection equipment. This provides the processing infrastructure needed to handle frozen vegetables at commercial scale.
From Raw Material Inspection to Finished Product
Quality control should begin before the corn enters the freezing stage.
A controlled production process may include:
- Raw-material inspection
- Washing and cleaning
- Sorting and grading
- Cutting or preparation according to specifications
- IQF freezing
- Metal detection and inspection
- Packing
- Cold storage
- Export shipment
Each stage contributes to the consistency of the finished product. Freezing, for example, cannot compensate for unsuitable raw materials or inconsistent preparation.
For international buyers, an integrated process also provides greater visibility into how the product is handled before shipment. This can be particularly valuable when purchasing recurring volumes and maintaining strict product specifications.
Frozen Sweet Corn Formats for Different Applications
Different food businesses may require different corn formats depending on their production process and final product.
IQF Sweet Corn Kernels
IQF sweet corn kernels are suitable for applications where individual kernels need to be portioned and incorporated directly into a formulation.
Common applications include ready meals, soups, salads, stir-fries, curries, pizza toppings, and other processed foods. The individual format is particularly convenient for food manufacturers and foodservice operations requiring flexible portion control.

Frozen Corn Cob Cuts
Corn cob cuts provide a more recognizable corn format and can be used where the appearance of the cob is part of the product presentation.
Uniform cutting is important for commercial applications because it helps create more predictable portion sizes and cooking performance.
Frozen Baby Corn
Frozen baby corn can serve applications where smaller, tender corn pieces are preferred. It is commonly relevant to stir-fries, mixed vegetables, ready meals, foodservice dishes, and other products where appearance and texture are important.
The appropriate format should ultimately be selected according to the final application, production method, packaging requirements, and target market.
Food Safety and Quality Control
For international buyers, food safety is a fundamental part of supplier qualification.
A professional frozen vegetable processor should have defined controls covering raw-material inspection, processing hygiene, foreign-material detection, product testing, packaging, storage, traceability, and shipment.
Relevant certifications and food-safety systems may include HACCP, ISO 22000, BRCGS, HALAL, and other requirements depending on the destination market and buyer specifications.
FUBA’s quality-control system includes food-safety management standards, metal detection, X-ray inspection, and in-house microbiological testing. These controls provide multiple inspection points throughout the production process and support the documentation requirements commonly associated with international procurement.
Cold-Chain Management and Shelf Life
Correct freezing conditions need to be maintained after processing. Frozen sweet corn should generally remain at ≤ -18°C during storage and transportation to help preserve its quality throughout the stated shelf-life period.
For international shipments, temperature control should cover the complete logistics chain, including loading, container transportation, customs handling, receiving, and warehouse storage.

Packaging also plays an important role. Appropriate inner and outer packaging helps protect the frozen product during handling while making it easier to store, stack, and distribute at commercial scale.
Buyers should confirm the supplier’s recommended storage temperature, shelf life, packaging configuration, and transportation requirements before finalizing an order.
Packaging Options for Buyers
Packaging requirements can vary significantly between importers, distributors, food manufacturers, foodservice operators, and retail businesses.
Manufacturers purchasing bulk quantities may prioritize larger cartons and food-grade inner liners for efficient warehouse handling. Foodservice businesses may require convenient bulk packs, while retail chains may need smaller consumer-ready formats with specific labeling and packaging requirements.
A supplier capable of providing different packaging formats can help buyers align the frozen product with their distribution model and reduce unnecessary repacking after import.
OEM and Customized Frozen Corn Specifications
Procurement often involves requirements beyond the basic product specification.
Depending on the buyer’s market and application, customization may involve:
- Kernel or piece specifications
- Cut size and format
- Packaging weight
- Inner and outer packaging
- Product labeling
- Private-label requirements
- Export documentation
OEM and private-label capabilities can be particularly useful for distributors and food brands that want to maintain their own packaging identity while sourcing directly from a processing facility.
For manufacturers, customization at the production stage can also reduce additional processing or repacking requirements after the product arrives in the destination market.

How to Evaluate a Frozen Sweet Corn Supplier Vietnam
Selecting a frozen sweet corn supplier Vietnam should involve evaluating the entire supply chain rather than focusing only on the quotation or product sample.
Raw Material Sourcing
Check whether the supplier has reliable access to suitable sweet corn and defined standards for maturity, quality, and incoming inspection.
Processing and Freezing Capability
Evaluate the supplier’s processing flow, IQF technology, freezing capacity, and ability to maintain consistent specifications across production batches.
Food Safety and Traceability
Confirm applicable certifications, testing procedures, traceability systems, and documentation required for your destination market.
Cold Storage and Logistics
Review storage temperatures, cold-storage capacity, packaging protection, and international transportation procedures.
Production and Supply Capacity
Consider whether the supplier can support your expected order volume, repeat purchases, and potential growth rather than only fulfilling a single shipment.
Communication and Customization
A suitable supplier should be able to communicate clearly about specifications, production schedules, packaging, documentation, and shipment planning.
Evaluating these factors together helps buyers distinguish a direct manufacturing partner from a trading intermediary and provides a more realistic picture of long-term supply reliability.
Why Factory-Direct Sourcing Can Benefit Buyers
Factory-direct sourcing can provide greater visibility across the supply chain because raw-material sourcing, processing, freezing, quality control, packaging, and storage are managed within the manufacturing operation.
This can make communication around technical specifications and production requirements more straightforward. It may also help buyers respond more efficiently when they need customized formats, packaging, or recurring production volumes.

For international buyers, the key benefit is not simply purchasing directly from a factory. It is having clearer control over the stages that determine product quality and supply consistency.
Conclusion
Selecting a frozen sweet corn supplier Vietnam is ultimately a supply-chain decision rather than a simple purchasing decision. Consistent raw materials, controlled processing, IQF freezing, food-safety systems, suitable packaging, cold storage, and reliable export logistics all contribute to successful long-term sourcing.
Vietnam provides a practical sourcing base for frozen sweet corn, but buyers should evaluate the supplier’s manufacturing capability and supply-chain controls rather than focusing solely on product origin or price.
For businesses looking to establish a stable supply relationship, a supplier with direct processing capabilities, appropriate freezing and inspection systems, reliable cold-chain infrastructure, and experience with international requirements can provide greater confidence across recurring orders.


